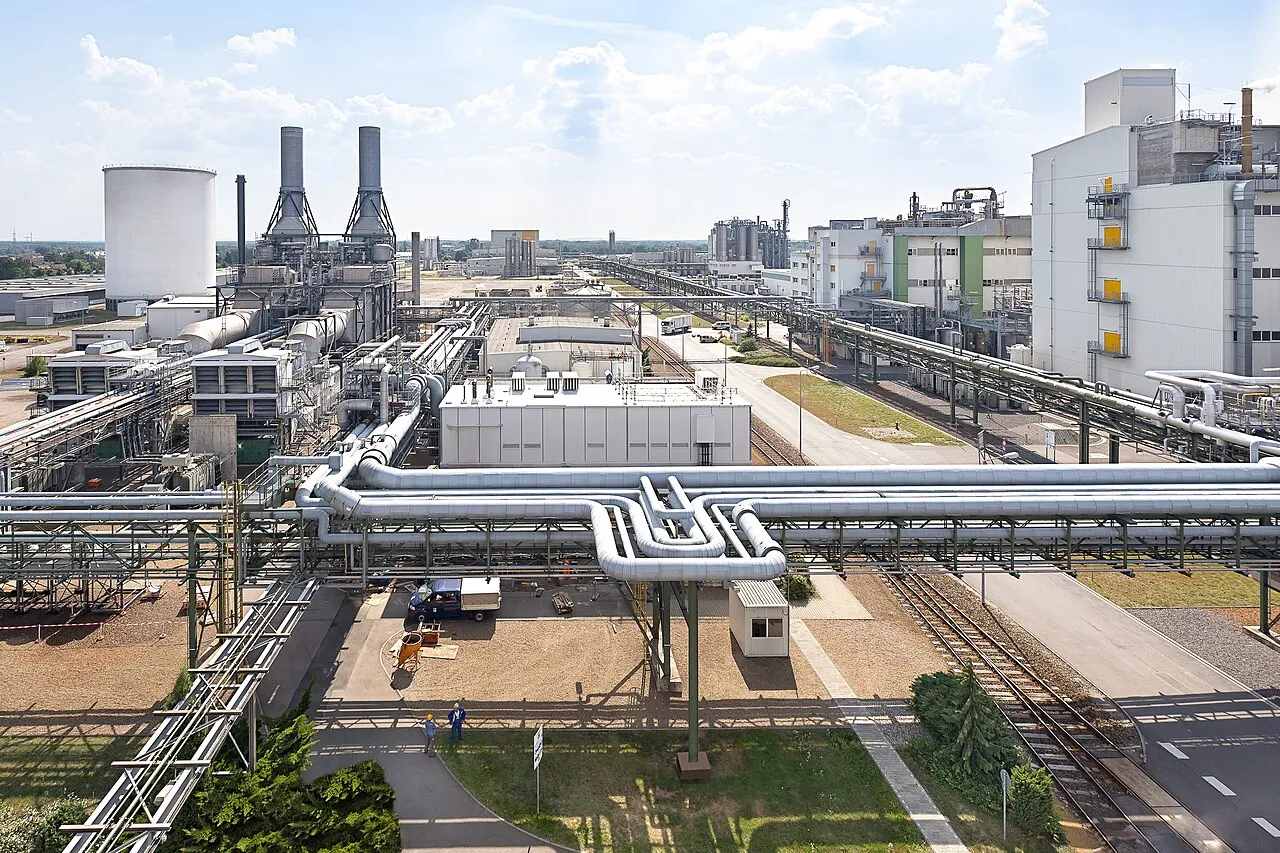
Chemical plant facilities operate as large-scale industrial complexes designed to manufacture and process chemical or biological materials into valuable new products. These specialized operations utilize advanced equipment and technology to transform raw feedstocks through complex chemical and physical transformations. While traditional chemical plants focus on commodity chemicals and petrochemicals, similar technological systems are shared across polymer production, oil refineries, and pharmaceutical manufacturing facilities.
The operational core of these facilities relies on detailed industrial-scale methods known as chemical processes. These processes can function either through continuous operation, where materials flow steadily to maximize efficiency in commodity manufacturing, or through batch operation, which offers greater flexibility and traceability for specialty and pharmaceutical production. Engineering these systems requires precise management of reaction kinetics, fluid dynamics, and thermodynamic constraints to ensure optimal output and safety.
Related Stories
Get the Latest Sports News from Seymour's Bird
Receive the latest updates on football, basketball,and technology news directly in your inbox. It's free!
SubscribeDesigning a modern chemical plant is a rigorous multidisciplinary endeavor led primarily by professional chemical engineers. From initial laboratory research by chemists to scaling up through pilot plants, engineers utilize block flow diagrams, material balances, and energy calculations to optimize plant capacity. Mechanical, electrical, and structural engineers also collaborate to ensure that the massive vessels, piping networks, and supporting structures withstand rigorous industrial operating conditions.
Safety, environmental constraints, and economic viability remain paramount throughout the lifecycle of any chemical facility. Cost studies serve as initial screening tools to evaluate commercial potential before projects advance to full-scale construction. By integrating advanced instrumentation, online analyzers, and rigorous maintenance schedules, modern chemical plants maintain high operational uptime while meeting strict regulatory and environmental standards.
Unit Operations and Fluid Systems in Industrial Plants
Unit operations form the foundational building blocks of chemical processing, representing specific physical or chemical steps such as filtration, distillation, and heat exchange. These operations take place within large cylindrical vessels or interconnected units designed to handle extreme temperatures and pressures. Specialized equipment like catalytic reactors and fluidized beds facilitate precise molecular transformations while managing reaction heat effectively.
Fluid systems play a critical vital role in transporting gases, liquids, and multi-phase mixtures throughout the facility via intricate networks of piping and tubing. Pumps and compressors pressurize and move these material streams, while specialized valves control flow rates dynamically. Insulation is heavily applied to high- and low-temperature equipment to guarantee personnel safety and maintain thermal equilibrium across all operational units.
Separation processes are equally crucial for achieving desired product purity levels depending on commercial specifications. Techniques such as fractional distillation, crystallization, extraction, and reverse osmosis allow operators to isolate target compounds from complex mixtures. Storage tank farms strategically hold raw feedstocks, intermediate products, and final outputs, equipped with advanced level indicators and monitoring instruments.
Instrumentation and automation have transformed plant operations by incorporating real-time temperature, pressure, and flow sensors. Modern facilities heavily rely on online analyzers to monitor chemical and physical properties continuously, ensuring stable steady-state conditions. This technological integration allows operators to maximize plant capacity safely while minimizing environmental impact and preventing unexpected operational disruptions.